


 Blogs

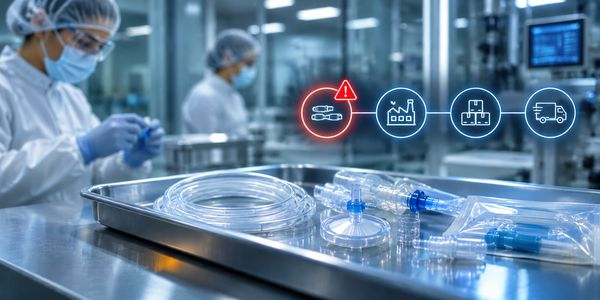
A single missing component can prevent a medical device from being completed and delivered to a hospital, even when every other material is available. The difficult question is rarely just how to find more stock. It is how to allocate constrained supply across products, plants and customers without creating a second disruption elsewhere.
Key Takeaways
- Shared components create hidden dependencies across product families, sites and customer commitments.
- Usable inventory is not the same as physical inventory: quality status, approved substitutions and market requirements affect availability.
- Scenario planning helps compare allocation, rescheduling and sourcing responses before scarce stock is committed.
- Constraint-based optimization can connect component allocation with production capacity, delivery priorities and business rules.
Why do component shortages create a chain reaction?
Medical devices often rely on multi-level bills of materials, specialized suppliers and tightly controlled production processes. A delayed connector, sensor, electronic board or sterile-packaging item may be shared across several finished products. When supply falls short, the impact travels through the bill of materials into production schedules, inventory commitments and customer deliveries.
Teams may see the same shortage differently. Procurement focuses on expediting the part, production focuses on line utilization, and commercial teams focus on protecting delivery promises. Each perspective matters, but optimizing them separately can produce a plan that looks reasonable locally and fails across the network.
 ICRON is a Major PlayerIDC MarketScape: Worldwide Supply Chain Planning 2026 in
Life SciencesClick to Learn More
What makes medical device allocation different from ordinary inventory allocation?
Not every component on hand is available for every use. Approved supplier status, product configuration, quality release, traceability, sterilization requirements and market-specific rules may limit which materials can be assigned to which orders. A substitute part cannot simply be used because it fits physically; appropriate engineering, quality and regulatory approval may be required.
This distinction is critical: the planning question is how much eligible, usable supply can support a feasible production and delivery commitment, not merely how much stock appears in the warehouse.
Four decisions that should be evaluated together
Which products and orders should receive scarce materials, considering service priorities, demand, commitments and approved eligibility?
Which plants and lines can actually build the selected products with available labor, tooling, changeover windows and materials?
Where should remaining stock be held or transferred to protect service across sites without creating excess elsewhere?
What changes if a supplier is delayed again, a qualified alternate becomes available, or demand shifts to another region?
How can scenario planning turn a shortage into a manageable decision?
Consider an illustrative manufacturer producing three device families that share a limited component. A first-come, first-served allocation might exhaust the component on a lower-priority product while delaying a time-critical order. Allocating only to the highest-margin device could also fail if the necessary assembly capacity or approved material configuration is unavailable.
A stronger response compares several feasible options: protect urgent orders, rebalance production across qualified sites, transfer eligible inventory, or adjust the build sequence. Each scenario should show its consequences for delivery commitments, resource use, cost and residual shortages. The objective is not to automate a simplistic priority rule, but to make trade-offs explicit and executable.
Where can ICRON help medical device manufacturers?
ICRON’s Life Sciences approach combines decision intelligence, scenario planning and constraint-aware optimization. In a medical device shortage, that can support the evaluation of scarce-component allocation across products and plants, production rescheduling around real resource constraints, and alternative inventory or network responses. Rather than treating each decision in isolation, planners can compare feasible combinations before approving a response.
AI-native decision execution is relevant where approved planning decisions need to move into governed workflows. AI-supported analysis can help identify exceptions and surface alternatives, while mathematical optimization generates component allocation and production scheduling decisions that balance service and cost objectives within defined material and capacity constraints. Human oversight remains important for quality, regulatory and business-critical decisions.
Industry research provides another lens for evaluating complex planning requirements. ICRON was positioned as a Major Player in the IDC MarketScape 2026 Life Sciences supply chain planning assessment and recognized in Gartner research covering discrete-industry supply chain planning and supply chain network design. These assessments concern vendor positioning and market coverage, not verified outcomes for medical device manufacturers. The practical test remains whether a planning approach can represent actual qualification, material, capacity and allocation constraints.
How should manufacturers measure the quality of a shortage response?
Useful measures include the number of critical orders protected, achievable on-time delivery, constrained-component utilization, production schedule stability, excess transfers, inventory exposure and the time needed to approve a revised plan. These measures should be considered together. Maximizing a single metric can shift the disruption rather than resolve it.
Facing complex planning trade-offs?
Every medical device supply chain has different constraints. Discuss how scenario analysis and constraint-based planning could help your team evaluate its options.
Frequently Asked Questions
How can manufacturers prioritize orders when a medical device component is scarce?
Compare customer and patient-service priorities with component eligibility, production feasibility, delivery commitments and business objectives. Test alternatives before allocating limited supply.
Can an alternate component be used immediately?
Not necessarily. Engineering, quality, regulatory and approved-supplier requirements may restrict substitutions, even where a part appears functionally similar.
How does scenario planning help?
It lets teams compare reallocating inventory, rescheduling production, shifting qualified capacity and adjusting delivery priorities, while showing the consequences of each option.
What is the role of AI in medical device supply chain planning?
AI can support exception detection and decision analysis; mathematical optimization generates component allocation and scheduling decisions based on defined service objectives and operational constraints. Decisions remain subject to business governance and required approvals.
From shortage visibility to executable choices
Better visibility reveals where the shortage is. Better planning reveals what can be done about it. For medical device manufacturers, the greatest value comes from linking material eligibility, production feasibility, inventory and service priorities into one decision process.
Read more about ICRON’s approach to life sciences planning →
Further reading: FDA Medical Device Shortages List · ICRON industry recognition · Life Sciences Supply Chain Planning guide